
Chemical Dosing Skids
Engineered chemical dosing skids integrate metering pumps, tanks, piping, valves, instrumentation and controls into one compact package designed around your process conditions.
From simple single-pump dosing systems to duty/standby and multi-chemical packages, each skid can be configured according to dosing rate, discharge pressure, chemical compatibility, control philosophy and project specifications.

Configuration starts with process data, not a fixed equipment list.
A Complete Dosing System Built Around Your Process
A chemical dosing skid is more than a pump mounted on a frame. It brings storage, metering, protection, monitoring and control together as one engineered package.

The final configuration depends on the chemical, dosing duty, operating pressure, control philosophy and required system availability.
Storage & Feed
Chemical storage or day tank, suction line, isolation valves, strainer and level monitoring.
Metering & Delivery
Metering pump, duty/standby arrangement, calibration column and chemical injection connection.
Pressure Protection
Pressure relief valve, back-pressure valve, pulsation dampener and pressure monitoring where required.
Instrumentation & Control
Flow or pressure monitoring, local control panel, PLC / HMI and plant communication according to project scope.
From Chemical Storage to Controlled Injection
A dosing skid should be engineered as one continuous process path. The pump is only one part of the system—the suction conditions, pressure protection, flow stability, monitoring and final injection all affect dosing performance.
Storage & Suction
Chemical is supplied from an integrated day tank or external storage system through a suction line designed for reliable pump feeding.
- Tank or bulk supply
- Isolation valve
- Level monitoring
- Suction strainer where suitable
Controlled Pumping
The metering pump delivers the required chemical flow against the process pressure according to the selected operating strategy.
- Fixed or variable output
- Simplex or duty/standby
- Stroke / speed adjustment
- Capacity matched to duty range
Protection & Stabilization
Pressure control and pulsation management protect the pump and help create more stable downstream dosing conditions.
- Pressure relief valve
- Back-pressure valve
- Pulsation dampener
- Pressure indication
Monitoring & Control
Instruments and controls can confirm pressure, flow and operating status before the chemical reaches the injection point.
- Flow monitoring
- Pressure transmitter
- PLC / HMI logic
- Alarm and interlock signals
Controlled Injection
The chemical enters the process at the specified injection point through the final connection or injection quill.
- Injection quill where required
- Process isolation
- Defined discharge pressure
- Final chemical delivery
The same process path can operate with different levels of automation.
The control method should match how much the process demand changes and how closely chemical addition must follow that change.
What We Need Before Sizing Your Chemical Dosing Skid
A useful RFQ should describe the chemical, the dosing duty, the process pressure and the control philosophy. The more complete the input data, the more accurately the skid can be configured.
Determines compatibility, pump behavior and wetted-material direction.
Defines the operating envelope instead of sizing only around one nominal point.
Defines storage philosophy, redundancy and the physical arrangement of the package.
Defines how the dosing rate responds to process demand and how the skid connects to the plant.
Prevents late-stage changes to inspection, testing and document scope.
How Dosing Capacity Is Sized
The theoretical dosing flow is only the starting point. Final pump selection should be checked against the full operating range, discharge pressure, chemical properties and the required control strategy.
Start With the Required Chemical Dose
For many liquid dosing applications, the initial solution flow can be estimated from:
Estimate the Theoretical Dosing Flow
Enter the three basic process values below. This calculator provides a preliminary result only and does not replace final pump selection.
Enter the process data above to calculate.
Do Not Size the Pump From One Nominal Flow Point
Minimum, normal and maximum duty should be reviewed together so the selected pump can operate within a practical control range.
Check minimum stable output, turndown and whether the control method can maintain the required low-flow condition.
The normal point should sit in a practical operating range instead of at an extreme end of the pump capacity.
Maximum flow should include the real process requirement and any justified operating margin without excessive oversizing.
The calculation must still be checked against the real operating conditions.
Injection pressure and line losses define the required pump discharge capability.
Tank level, suction lift, piping arrangement and chemical behavior affect pump feeding.
Density, viscosity, concentration and off-gassing behavior can change the selection.
The selected pump should cover the required operating range with usable control.
Critical service may require duty/standby or other availability arrangements.
Manual, pulse, 4–20 mA, flow-paced or analyzer control affects how capacity is managed.
Selecting a pump only from the normal dosing rate can create poor turndown, unstable low-flow operation or insufficient capacity at peak demand.
Select the Pump From the Full Operating Duty
Pump selection should consider flow, discharge pressure, chemical properties, viscosity, turndown, accuracy and required system availability together—not as separate decisions.
Six engineering questions should be answered before the pump is fixed.
The full range determines capacity and usable turndown.
Process pressure and line losses define discharge capability.
Chemical compatibility defines the wetted-material direction.
Higher viscosity can change pump and suction arrangement.
Manual, pulse, 4–20 mA or process feedback affects control range.
Critical service may justify duty/standby or additional redundancy.
Select an operating condition to see the main design focus.
This is not an automatic pump specification tool. It is a quick way to show which engineering factor normally becomes more important under different operating conditions.
Metering diaphragm pump
A metering diaphragm pump is a common engineering direction where controlled liquid dosing and repeatable adjustment are required.
- Primary focus
- Dosing accuracy and controllability
- Check carefully
- Turndown and low-flow stability
- Typical controls
- Manual, pulse, 4–20 mA or variable speed
High-pressure metering arrangement
Higher discharge pressure may move the selection toward a hydraulic diaphragm or other suitable high-pressure metering-pump arrangement.
- Primary focus
- Discharge-pressure capability
- Check carefully
- Relief setting, piping class and injection pressure
- Typical controls
- Capacity control matched to pump technology
Chemical-compatible diaphragm and wetted materials
Chemical compatibility can become the controlling selection factor. Pump head, diaphragm, valves, seals and connecting piping must be reviewed together.
- Primary focus
- Wetted-material compatibility
- Check carefully
- Concentration and operating temperature
- Typical controls
- Selected independently from material choice
Pump with practical output control range
Where dosing demand changes with plant flow or analyzer feedback, the pump should provide usable modulation across the required duty range.
- Primary focus
- Turndown and response to changing demand
- Check carefully
- Minimum stable output
- Typical controls
- 4–20 mA, pulse or flow-paced signal
Duty / standby pump arrangement
Where interruption of chemical dosing could affect plant operation, redundancy should be considered as part of pump selection rather than added after the skid is designed.
- Primary focus
- System availability
- Check carefully
- Automatic or manual changeover philosophy
- Typical controls
- Duty selection, failure alarm and standby start
Suction system and pump technology need reassessment
Higher viscosity can increase suction losses and reduce filling performance. Pump selection cannot be separated from suction-line design.
- Primary focus
- Reliable pump filling
- Check carefully
- Suction size, length and static head
- Typical controls
- Defined after hydraulic review
Typical requirement versus engineering direction
API 675 can be relevant for controlled-volume reciprocating positive-displacement metering pumps in applicable industrial service. It should not be presented as a universal requirement for every chemical dosing skid.
Every Accessory Should Solve a Defined Operating Problem
A dosing skid should not include accessories simply because they appear on a standard equipment list. Each component should have a clear function linked to the pump, pressure conditions, chemical behavior or control requirement.
Protect the pump and discharge piping from excessive pressure.
Provides a defined pressure-relief path if the discharge side becomes blocked or pressure rises above the intended operating limit.
Commonly considered where a positive-displacement metering pump can generate pressure against a closed or restricted discharge path.
Excessive pressure can damage the pump, valves, tubing, piping or other downstream components.
Maintain stable discharge conditions when process pressure alone is not enough.
Creates a controlled minimum discharge pressure so the metering pump operates against a more stable hydraulic condition.
Useful where the injection point has low, changing or insufficient back pressure for consistent metering performance.
Unstable discharge conditions can affect dosing repeatability and may contribute to siphoning or uncontrolled flow in some layouts.
Reduce the pressure and flow pulsation created by reciprocating metering pumps.
Absorbs part of the cyclic pressure variation produced during the pump stroke and reduces downstream pulsation.
Consider where pulsation may affect piping, pressure instruments, flowmeters or process stability.
Higher pulsation can increase vibration, unstable readings and pressure peaks in downstream equipment.
Provide a practical way to verify actual pump delivery.
Allows operators or commissioning personnel to measure the volume drawn by the pump over a known time period.
Useful during commissioning, maintenance or routine verification where actual delivered flow needs to be checked locally.
Actual pump delivery may be harder to verify against the setpoint without separate test equipment or instrumentation.
Make the real discharge condition visible to operators and controls.
Provides local indication or a remote pressure signal for monitoring, alarms, diagnostics or interlocks.
Important where pressure changes can indicate blocked injection, valve problems or abnormal system operation.
Pressure-related faults can be more difficult to detect, diagnose and integrate into the control philosophy.
Confirm that chemical flow is actually being delivered.
Provides flow indication, confirmation or measurement downstream of the metering pump where dosing verification is required.
Useful for critical dosing, automated alarm logic, performance verification or processes where pump status alone is not enough.
A running pump does not always guarantee that the expected chemical flow is reaching the process.
Introduce the chemical at the intended location inside the process line.
Positions the chemical entry point within the process line instead of discharging directly at the pipe wall.
Consider where injection location, mixing, wall exposure or process-line geometry affects dosing performance.
Poor injection location can reduce mixing quality or expose the pipe wall to concentrated chemical.
Protect the pump inlet where debris protection is appropriate.
Helps prevent suitable particulate contamination from reaching pump check valves or other sensitive inlet components.
Used where contamination risk exists and where the chemical and suction conditions are compatible with a strainer.
Debris may interfere with check-valve sealing or pump performance if upstream contamination is possible.
Specify the operating problem first, then select the component that solves it.
More accessories do not automatically mean a better skid. The correct arrangement is the one that addresses the real hydraulic, chemical, monitoring and maintenance requirements of the dosing duty.
Tank Size Should Follow the Operating Philosophy
Tank selection should not start from an arbitrary volume. A better starting point is how much chemical the process consumes and how long the skid should operate between refills.
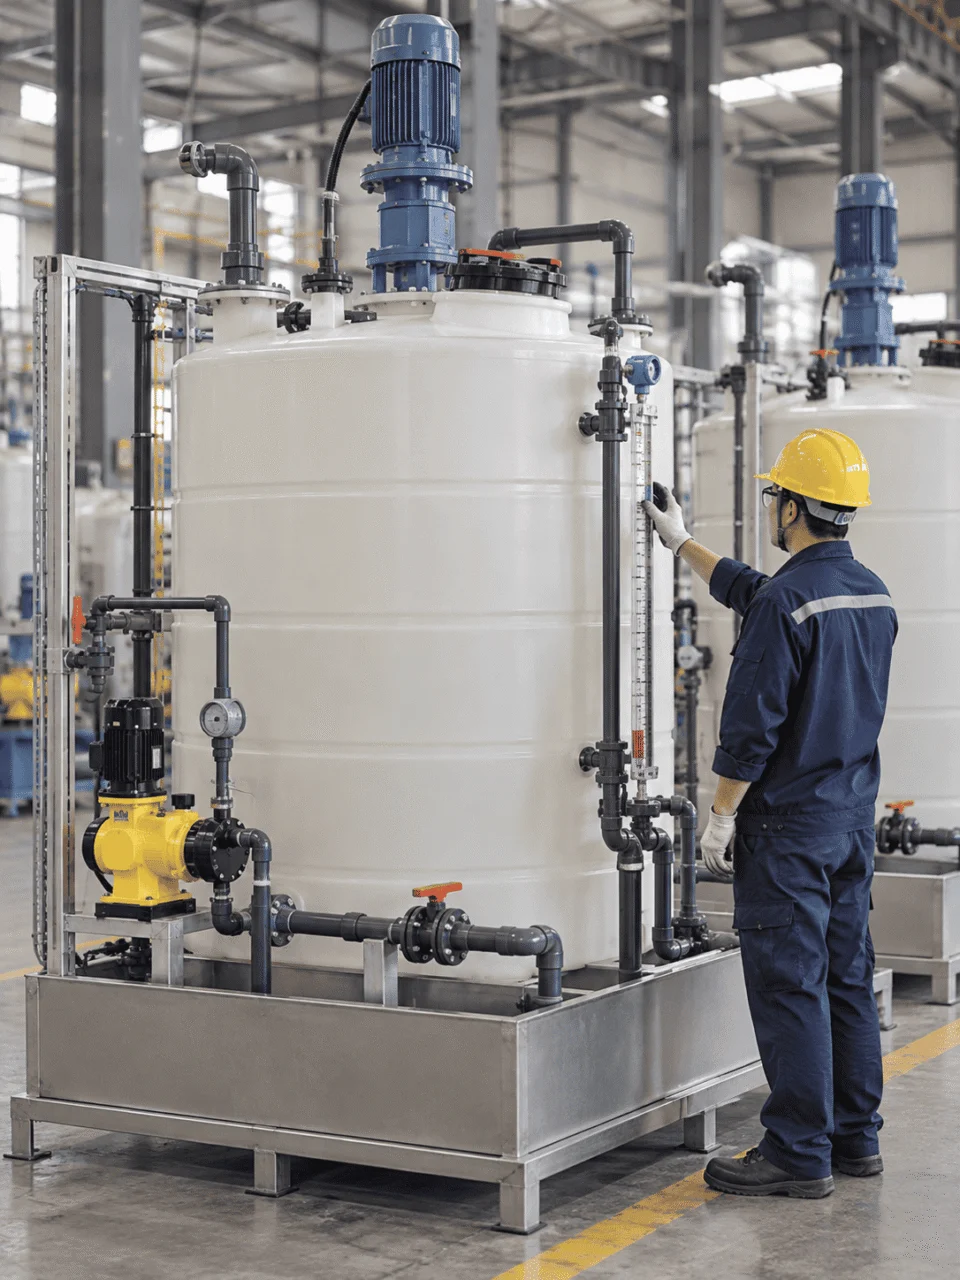
Storage volume, refill frequency, usable level range and mixing requirements should be reviewed as one operating system.
Start With Required Operating Autonomy
The preliminary volume should then be adjusted for the usable level range, minimum operating level, dead volume, refill method and any project-specific operating margin.
Refill frequency affects the required storage autonomy and whether an integrated day tank or external bulk supply is more practical.
Nominal vessel capacity is not the same as usable operating volume. Minimum level, freeboard and dead volume should be considered.
High / low switches, continuous level measurement and pump interlocks can be incorporated according to the operating philosophy.
Mixing should be included only when the chemical preparation, dilution, suspension behavior or process requirement justifies it.
Storage, dosing and controls assembled as one package.
Skid receives chemical from a separate storage system.
Used where preparation or continuous mixing is required.
Separate storage circuits for different chemicals or duties.
Do Not Add a Mixer Automatically
A mixer adds equipment, controls, maintenance and power consumption. It should be specified because the chemical or preparation method requires it—not simply because the skid includes a tank.
Mixing may be needed to achieve a consistent concentration before dosing.
Agitation may be required to maintain a reasonably uniform suspension.
Mixing duty should then be defined as part of the tank design basis.
No preparation step may be required before the pump suction.
Additional agitation may not improve dosing performance.
Mixing responsibility may already be handled by the upstream storage system.
Can be used for refill control, alarm or overfill prevention logic.
Can provide operator warning before the tank reaches the minimum usable level.
Can be used to stop the dosing pump where dry-running protection is required.
Connections should match filling, maintenance, chemical behavior and containment philosophy.
Material Selection Requires More Than the Chemical Name
Wetted materials should be reviewed against the complete service condition. Chemical concentration, temperature, pressure and exposure mode can change whether a material remains suitable.
Identify the actual chemical or solution being dosed.
Check the real operating concentration, not only the chemical name.
Review both normal and credible maximum operating temperatures.
Consider pressure, continuous contact and mechanical duty.
Confirm the final wetted-material combination for the complete skid.
The same chemical can create a different material-selection problem when the service condition changes.
A material that performs acceptably at one concentration may not remain suitable when the solution becomes more concentrated or diluted.
Higher temperature can accelerate corrosion, soften some polymers or reduce the allowable mechanical duty of a material.
Chemical resistance alone is not enough if the material also has to withstand pressure, vibration, piping loads or repeated maintenance.
Continuous immersion, intermittent contact, vapor exposure and splash conditions can require different engineering judgement.
Common material families that may enter the evaluation
This list is not a compatibility chart. Final selection must be checked against the exact chemical, concentration, temperature, pressure and component duty.
Every wetted component must be reviewed—not only the tank and main piping.
A skid can still fail a compatibility review if one small wetted component is overlooked. Material verification should therefore cover the complete chemical path.
Check the head material, diaphragm material, valve balls, seats and internal wetted parts.
Review both chemical compatibility and the required mechanical pressure rating.
Body material alone does not confirm compatibility if internal soft parts differ.
Diaphragms, sensor bodies and process connections must match the chemical service.
Tank material, mixer wetted parts and level instruments should be checked as one assembly.
The last components before the process line remain part of the chemical-contact path.
From Manual Dosing to Closed-Loop Process Control
The control philosophy should match how much the process demand changes, how quickly the dosing rate must respond and how much operating visibility the plant requires.
More automation should solve a real process need—not simply add complexity.
Suitable where process demand remains relatively stable.
The operator sets the pump output locally using stroke length, speed or another pump adjustment method. This is the simplest control philosophy.
Useful where frequent automatic correction is not required.
No continuous external process signal is required.
Operators must manually adjust the dosing rate when conditions change.
Pump output responds directly to an external control signal.
This arrangement is useful where another instrument or controller already determines the required dosing command.
Useful where the plant already provides a proportional control signal.
The pump follows the external command within its usable control range.
The pump must remain stable across the commanded operating range.
Chemical addition tracks the main process flow.
The dosing rate changes as the process flow changes, helping maintain a more consistent chemical dose per unit of process flow.
Common where the target dose is linked directly to the process flow rate.
The control system scales pump output against the measured plant flow.
It follows flow, but does not directly measure whether the treatment target was achieved.
Dosing responds to a measured process condition.
Analyzer feedback can be used where the actual process result should influence chemical addition instead of relying on flow alone.
Other process analyzers can also be integrated where appropriate.
Useful where the target process condition must be maintained automatically.
Poor measurement quality or aggressive tuning can create unstable control behavior.
The dosing skid becomes part of the plant control architecture.
More complex packages can manage pump sequencing, alarms, interlocks, level logic, automatic changeover and remote plant communication.
Local automation can be combined with plant-level communication.
Useful where operators need centralized status, alarms and control.
Late control changes can affect wiring, instruments, panel design and FAT scope.
A typical signal path from field condition to plant response
Define the signals before the panel and wiring are finalized.
Automation should be defined before fabrication. Instruments, alarms, interlocks, communication signals and fail-safe actions all affect the skid wiring, control panel, documentation and FAT scope.
Configure the System Around Process Criticality
The right skid arrangement depends on required availability, maintenance philosophy, number of chemicals, storage strategy and how much interruption the process can tolerate.
One metering pump for one dosing duty.
A simplex arrangement is the most direct configuration where one pump can satisfy the required dosing duty and process interruption is acceptable during maintenance or pump replacement.
One pump operates while the second remains available.
This arrangement improves system availability where chemical dosing should continue during pump maintenance, failure or planned changeover.
Use additional pumps to extend capacity and preserve redundancy.
This arrangement can be useful where one pump cannot cover the full peak duty efficiently, or where the system needs both capacity staging and a standby unit.
Multiple dosing pumps integrated on one common skid.
Several pumps can serve separate injection points, parallel duties, different capacities or staged operating requirements while sharing part of the skid infrastructure.
Several independent chemical circuits on one engineered package.
Multi-chemical systems require separation between chemical circuits, individual compatibility review and a clear approach to containment, controls and maintenance access.
Storage, dosing and controls combined into one package.
An integrated day tank can simplify installation where the required operating autonomy fits within the available skid footprint.
Receive chemical from an external storage system.
A tankless skid focuses on pumping, protection, instrumentation and control while chemical storage is handled elsewhere in the plant.
Add environmental protection where the installation requires it.
Outdoor, cold-weather, high-temperature or exposed installations may require an enclosure, ventilation, heating, insulation or other environmental provisions.
Use process criticality to narrow the arrangement
One pump, lower complexity, maintenance requires dosing interruption.
Redundancy added where dosing availability matters to plant operation.
Capacity staging combined with standby coverage.
Several dosing circuits integrated on one engineered skid.
Design the Skid for Abnormal Conditions, Not Only Normal Operation
A chemical dosing system should answer two questions: how does it operate when everything is normal, and what should happen when pressure, level, flow, leakage or equipment status moves outside the intended condition?
Risk → Detection → Protective Response
Safety provisions should be linked to a defined failure mode. This avoids adding hardware without a clear purpose and helps define the control and interlock philosophy before fabrication.
Leakage, low chemical supply, blocked discharge, pump failure or abnormal environment.
Level switch, pressure transmitter, flow monitor, leak sensor or equipment fault signal.
Alarm, stop the pump, change to standby, isolate the system or notify the plant control system.
Select a condition to review the typical protection strategy.
Contain the release and detect it before it becomes a larger plant issue.
Secondary containment or a bunded skid base should be sized and arranged according to the chemical inventory, project requirement and drainage philosophy.
Prevent loss of chemical supply from becoming an uncontrolled pump condition.
Alarm levels should be coordinated with the real usable tank volume and the time required for an operator or chemical-delivery action.
Protect the positive-displacement pump and downstream piping from blocked discharge.
Relief settings, alarm levels and trip thresholds should be coordinated with pump capability, normal operating pressure and piping design limits.
Do not assume that a running pump always means chemical is reaching the process.
Flow monitoring can provide a stronger confirmation of chemical delivery than pump run status alone where the dosing duty is critical.
Define how the system should behave when the operating pump becomes unavailable.
The required response depends on whether the process can tolerate dosing interruption and whether automatic standby operation is included in the control philosophy.
Electrical and instrumentation requirements must match the classified installation area.
Hazardous-area requirements should be defined during the RFQ stage because they can affect motors, instruments, junction boxes, panel design and documentation.
Use several protection layers instead of relying on one device.
Materials, pressure ratings and pump selection should suit the intended service.
Bunded bases, trays or other containment provisions limit the spread of a release.
Level, pressure, flow and leak signals identify abnormal operating conditions.
Control logic defines what the skid should do when an abnormal condition is detected.
Possible provisions depending on the chemical and project
Safety provisions should be defined from the chemical hazard, installation environment and project requirements. The goal is not to add every possible protection device—it is to create a clear, justified response to credible failure conditions.
Chemical Dosing Skids for Different Industrial Processes
The same basic dosing principle can serve very different industries, but the chemical, pressure, materials, hygiene requirements, controls and documentation should be reviewed for the actual process duty.

Chemical Processing
Controlled addition of reactants, catalysts, inhibitors, neutralizing agents and other process chemicals.
View Industry
Petrochemical
Dosing packages for treatment chemicals, corrosion inhibitors and process additives under project-specific operating conditions.
View Industry
Oil & Gas
Chemical injection duties where pressure, redundancy, materials and hazardous-area requirements can become critical design inputs.
View Industry
Pharmaceutical
Controlled chemical addition for suitable process and utility duties where project hygiene and documentation requirements apply.
View Industry
Food & Beverage
Dosing systems for compatible process, cleaning and utility chemical duties where material and hygienic requirements must be considered.
View Industry
Dairy
Chemical dosing for compatible cleaning, treatment and utility systems where sanitary process practices are part of the project basis.
View Industry
Brewing & Fermentation
Dosing packages for treatment, cleaning and compatible process-support chemicals used around brewing and fermentation systems.
View Industry
Water Treatment
Coagulants, disinfectants, pH adjustment chemicals, antiscalants and other treatment chemicals added according to the process requirement.
View Industry
New Energy
Project-specific dosing systems for process chemicals, treatment duties and supporting utility systems in new-energy facilities.
View IndustryA Chemical Dosing Skid Is Also an Engineering Package
For industrial projects, the deliverable is not only the physical skid. Drawings, datasheets, inspection records, testing and final documentation should be defined together with the equipment scope.
Define the documentation path before fabrication begins.
Process data, project specifications and purchaser requirements are reviewed first.
P&ID, GA, datasheets, material lists and control documents are developed.
Fabrication, assembly and inspection follow the approved project basis.
Functional checks, inspection points and agreed testing are completed.
Approved drawings, test records and operating documents are compiled for delivery.
Documentation scope should match the project—not a generic checklist.
Agree the FAT scope before the skid reaches the end of fabrication.
Confirm that the assembled skid matches the approved project basis.
Check pumps, tanks, valves, instruments and major accessories against approved documents.
Check physical arrangement, access, interface locations and major dimensions.
Confirm project tags and equipment identification where specified.
Verify the integrity and functionality of the assembled process path.
Review installed piping, supports, valves, connections and accessible maintenance points.
Confirm manual valve accessibility and intended flow-path operation.
Perform agreed testing where applicable to the project and component design.
Verify that the skid responds as intended before shipment.
Check installed instruments, ranges, signal response and basic functionality where applicable.
Simulate agreed operating conditions to verify control logic and protective responses.
Confirm pump operation, rotation, basic command response and duty/standby logic where included.
Make the FAT traceable instead of leaving it as an informal workshop check.
Document completed checks, measured values and agreed test results.
Record any open items and define how they will be closed before shipment.
Confirm the final drawing and document package reflects the delivered skid configuration.
Define who needs to witness or approve each step.
Depending on the project, inspection can be completed internally, witnessed by the purchaser or supported by third-party inspection. The required hold and witness points should be agreed before fabrication.
Internal inspection and test records according to the agreed project scope.
Customer or representative witnesses agreed FAT activities before shipment.
Independent inspection or witness points can be incorporated where specified.
FAT and documentation requirements should be defined during the RFQ and engineering stages. Leaving them until the end can create rework, missing records and delays to final acceptance.
What to Check Before Issuing a Purchase Order
Many dosing problems begin before fabrication. Incomplete process data, unclear control scope or selecting equipment from one nominal duty point can create redesign, poor turndown and late project changes.
Specify the engineering requirement—not just the equipment name.
The pump may operate poorly at minimum demand or lack capacity when the process reaches its maximum dosing requirement.
Specify minimum, normal and maximum dosing flow together with the required control range.
Pump selection, relief settings, piping pressure class and accessory configuration all depend on the real discharge condition.
State both normal and maximum injection pressure, including known downstream restrictions where available.
Concentration and temperature can change material compatibility even when the chemical name stays the same.
Provide chemical name, concentration, operating temperature and any client-specified wetted-material restrictions.
A single-pump package can create an unacceptable process interruption if dosing must continue during maintenance or equipment failure.
Define whether the duty is simplex, duty/standby or another arrangement, and whether changeover should be manual or automatic.
Excessive oversizing can reduce usable turndown and force the pump to operate near the bottom of its controllable range.
Require the proposed pump to demonstrate suitable operation across the specified minimum-to-maximum duty range.
Long suction lines, high viscosity, gas-forming chemicals or poor tank elevation can affect pump filling even when the discharge sizing is correct.
Provide tank location, suction elevation, approximate line length, viscosity and any known off-gassing behavior.
Late changes to alarms, interlocks, plant communication or automatic changeover can affect instruments, wiring, panel design and FAT scope.
Define the required control signal, PLC / HMI scope, I/O philosophy and DCS / SCADA interface during the RFQ stage.
Testing, witness points and records may require equipment access, simulation capability or documentation that cannot be added efficiently later.
State FAT, purchaser witness, TPI and documentation requirements before engineering approval and fabrication.
How complete is your dosing-skid specification?
Tick the information you already have. The percentage is only a planning aid, but it helps identify where the RFQ still needs engineering input.
Start with the chemical, dosing duty, pressure and control requirements.
Four questions that should have clear answers
Check minimum, normal and maximum duty—not only one nominal point.
Confirm concentration, temperature, pressure and wetted-component compatibility.
Confirm the control philosophy before panel fabrication and FAT planning.
Make sure the project deliverables are defined before the order is released.
A lower equipment price does not compensate for a skid that is incorrectly sized, difficult to control or missing critical project requirements. Compare suppliers on the completeness of the engineering scope, not only the pump model.
Frequently Asked Questions About Chemical Dosing Skids
These questions cover the points that most often affect sizing, pump selection, materials, controls, redundancy and project scope before a chemical dosing skid is released for fabrication.
Use the FAQ to confirm the basic engineering direction.
For final configuration, the actual chemical, concentration, dosing range, discharge pressure, suction conditions, controls and project requirements should still be reviewed together.
A chemical dosing skid is a packaged system that integrates the equipment required to store, meter, control and inject chemicals into an industrial process. Depending on the design, it may include tanks, metering pumps, piping, valves, instrumentation, controls and containment.
Sizing starts with the required chemical dose, process flow, chemical concentration and injection pressure. Minimum, normal and maximum dosing rates should then be checked against pump turndown, suction conditions, material compatibility and the required redundancy.
The most useful information includes chemical name, concentration, density, viscosity, minimum / normal / maximum dosing rate, injection pressure, process flow, temperature, tank requirement, pump arrangement, wetted materials, control philosophy, electrical supply and applicable project specifications.
A single pump can be suitable for non-critical or intermittent service. Duty / standby arrangements are usually considered where continuous chemical dosing is important to process operation or where maintenance downtime must be minimized.
Possible wetted materials may include 316L stainless steel, PP, PVC, CPVC, PVDF, PTFE, PE and other project-specific materials. Final selection depends on the chemical, concentration, temperature, pressure and mechanical duty of each component.
A back-pressure valve maintains a controlled minimum pressure at the metering pump discharge where the process does not naturally provide sufficient or stable back pressure for reliable dosing.
Reciprocating metering pumps produce pulsating flow. A pulsation dampener can reduce pressure variation and improve the stability of downstream piping, instruments and flow measurement where pulsation is significant.
Yes. Depending on the application, pump output can respond to pulse signals, 4–20 mA signals, process flow, analyzer feedback or PLC logic. More complex packages can also include automatic duty / standby changeover, alarms, interlocks and remote plant communication.
Where the project specification and operating service require it, suitable metering pumps manufactured to applicable API 675 requirements can be incorporated. API 675 should be treated as a project or pump specification requirement rather than a universal requirement for every chemical dosing skid.
Yes. Where specified, operating signals, alarms, status feedback, remote commands and setpoints can be integrated with the plant control system according to the agreed I/O list and communication philosophy.
No. A dosing skid can include an integrated day tank, or it can be designed as a tankless package receiving chemical from an external bulk storage system. The best arrangement depends on storage autonomy, available footprint and plant chemical-handling philosophy.
No. Mixing should be included only where the chemical preparation, dilution, suspension behavior or process specification requires it. A stable ready-to-dose liquid may not need continuous agitation.
Depending on the agreed scope, FAT may include equipment verification, piping inspection, valve operation, instrument checks, pump function, alarms, interlocks, control logic, leak or pressure testing where applicable, and review of the project documentation.
Depending on project scope, documentation can include P&ID, general arrangement drawings, equipment and instrument datasheets, BOM, valve and instrument lists, electrical drawings, I/O list, control philosophy, test records, material certificates and O&M documentation.
Send Us Your Chemical Dosing Requirements
The best dosing skid starts with accurate process data. Send us the chemical, concentration, dosing range, injection pressure, materials, controls and any available datasheet or P&ID.
If some inputs are not yet available, send what you have. The missing design information can be identified during the engineering review.