
Custom Shell and Tube Heat Exchangers
ChannelVessel designs and manufactures custom shell and tube heat exchangers for heating, cooling, condensation and heat-recovery duties across industrial process systems.
Fixed tubesheet, U-tube and floating head configurations can be engineered around the actual service conditions, with carbon steel, stainless steel and project-specified material combinations available according to the application.
We do not size an exchanger from heat-transfer area alone. Each design is reviewed around heat duty, temperature program, fluid properties, allowable pressure drop, fouling tendency, corrosion conditions, cleaning method, thermal expansion, design pressure and design temperature.

What Defines the Exchanger
Start With the Process, Not the Exchanger Type
The exchanger configuration should be the result of the process conditions — not the starting point.
Two shell-and-tube heat exchangers with similar heat-transfer area can require completely different internal arrangements because the fluids, operating pressures, fouling tendency, thermal expansion and cleaning requirements are different.
Do not force the process into a preferred exchanger type.
Which side operates at the higher pressure?
Placing a high-pressure stream on the tube side can often reduce the amount of material required to contain the pressure compared with designing a large-diameter shell for the same condition.
Which fluid is more likely to foul?
A fluid that leaves deposits may need direct access for mechanical cleaning. That requirement can influence whether it belongs inside straight tubes, whether the bundle must be removable and whether a U-tube arrangement is practical.
What kind of cleaning access is actually required?
“Cleanable” is not one condition. Tube-side access, shell-side access, chemical cleaning, mechanical tube cleaning, bundle removal and access to the outside of the tubes are different maintenance requirements.
How different are the shell-side and tube-side temperatures?
The shell and tubes expand independently as their temperatures change. When differential movement becomes significant, the mechanical configuration must be able to accommodate it.
How much pressure drop is actually available?
Higher velocity can improve heat transfer, but the same change also consumes more pressure drop. A practical design has to balance heat-transfer performance, hydraulic limits and long-term operating behavior.
Fixed Tubesheet, U-Tube or Floating Head?
There is no universally “best” shell-and-tube arrangement. Each configuration trades fabrication simplicity, cleaning access, thermal expansion capability and maintenance requirements differently.
Fixed Tubesheet
Mechanically straightforward construction with the tubesheets fixed to the shell.
- The fluids are relatively clean
- Shell-side mechanical cleaning is not a major requirement
- Temperature differences can be managed within the mechanical design
- A simpler construction is preferred
Straight tubes can provide convenient tube-side cleaning access, but the tube bundle is normally not removable. Shell-side deposits may therefore require chemical cleaning or another maintenance method.
U-Tube
The tube bundle can accommodate thermal movement through the U-bend geometry.
- Differential thermal expansion is important
- Shell-side access is required
- A removable-bundle arrangement is desirable
- The service is compatible with U-bend cleaning limitations
In common removable-bundle U-tube configurations, shell-side access can be good, but mechanical cleaning through the U-bend is more difficult than cleaning a straight tube from end to end.
Floating Head
One end of the tube bundle is allowed to move relative to the shell.
- Differential thermal expansion is significant
- Shell-side mechanical access is important
- The bundle must be removable
- Straight-tube cleaning access is required depending on the rear-head arrangement
Floating-head exchangers can provide strong maintenance flexibility, but they contain more components and sealing interfaces than simpler arrangements.
Compare the Design Consequences
| Design Question | Fixed Tubesheet | U-Tube | Floating Head |
|---|---|---|---|
| Differential expansion | Requires evaluation | Strong flexibility | Strong flexibility |
| Tube-side mechanical cleaning | Good with suitable head | Limited through U-bend | Good depending on head |
| Shell-side mechanical access | Limited | Good with removable bundle | Good |
| Bundle removal | Normally no | Commonly available | Yes |
| Construction complexity | Lower | Medium | Higher |
| Maintenance flexibility | Lower | Medium | Higher |
Can You Actually Pull the Bundle Out at Site?
A drawing may show a removable bundle. The installation may not. Extraction space has to be reviewed together with piping, platforms, structural steel, walls and lifting access.
If the bundle requires several metres of pull space but the plant provides only a narrow service corridor, the exchanger may be technically removable and practically impossible to maintain.
Which Fluid Should Go on the Tube Side?
Tube side or shell side is not decided by one rule. Pressure, corrosion, fouling, viscosity, phase change and allowable pressure drop have to be considered together.
Often Favored When Containment or Cleaning Drives the Decision
Smaller tube diameters can make pressure containment more practical, and straight tubes can provide direct mechanical cleaning access when the channel arrangement allows it.
Often Favored When Distribution, Phase Change or Geometry Benefits
Shell-side flow can be useful where crossflow, vapor handling, condensation, boiling or a larger flow area better suits the process conditions.
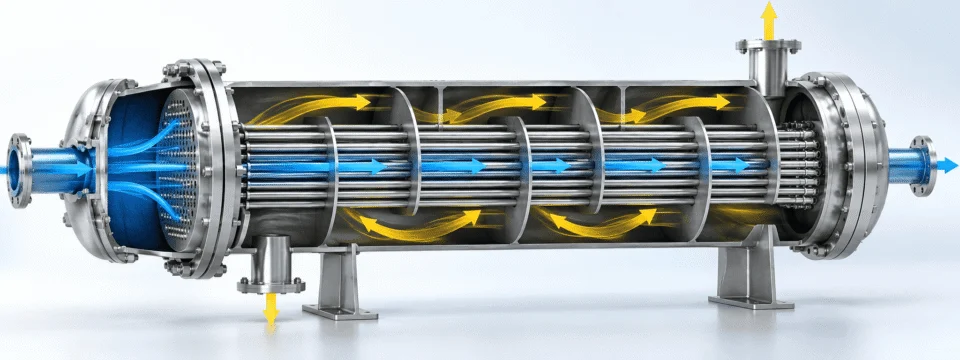
High-pressure streams are frequently considered for the tube side.
The smaller tube diameter can make pressure containment more practical than pressurizing a much larger shell.
A corrosive stream may be placed where expensive alloy use can be controlled.
When only one process stream requires a costly corrosion-resistant material, tube-side allocation can sometimes reduce the total amount of alloy required.
Decide how deposits will be removed before deciding the flow path.
Straight tube-side passages can offer direct mechanical cleaning access. A heavily fouling stream placed where access is poor can turn a thermally successful exchanger into a maintenance problem.
Viscosity changes the hydraulic and thermal picture.
It affects velocity, Reynolds number, pressure drop and heat-transfer behavior. Generic “put the viscous fluid here” rules can fail when the full operating conditions are ignored.
Phase change introduces another design layer.
Condensation or boiling can change the preferred side because fluid distribution, drainage, vapor disengagement, pressure drop and orientation become part of the design problem.
Velocity, Fouling and Pressure Drop Have to Be Balanced Together
More velocity is not always better. Less pressure drop is not always better. The exchanger has to reach the required duty without creating a hydraulic, fouling or mechanical penalty.
If Velocity Is Too Low
Weak surface shear can encourage deposit accumulation in some services. Poor distribution can also leave part of the exchanger surface underutilized.
The Target Is a Balanced Operating Range
The objective is to establish a flow condition that delivers the required heat-transfer performance while staying within the process pressure-drop limit and avoiding unnecessary fouling, erosion or vibration risk.
If Velocity Becomes Excessive
Pressure loss can become unacceptable. Depending on the fluid and exchanger geometry, high local velocities may also increase erosion risk or contribute to flow-induced vibration.
More Heat-Transfer Area Can Reduce Velocity
Adding more tubes increases surface area. But if the same process flow is divided through substantially more parallel flow area, tube-side velocity can fall.
Baffle Design Changes More Than the Flow Direction
Baffles guide shell-side flow across the tube bundle, but they also change velocity, pressure drop, flow distribution, tube support and vibration behavior.
Spacing, cut, leakage paths and unsupported tube length should be reviewed together.
Spacing changes shell-side crossflow velocity.
Closer spacing can increase shell-side velocity and heat transfer, but it also increases pressure drop and changes tube support conditions.
The open area changes how fluid crosses the bundle.
Too much or too little window area can alter crossflow velocity, hydraulic resistance and the distribution of shell-side flow.
Real shell-side flow is not perfectly ideal.
Leakage paths, bypass streams, bundle clearances and local geometry affect how much fluid actually crosses the active tube field.
Baffle geometry also affects vibration behavior.
Shell-side velocity, unsupported tube span and local flow pattern should be reviewed together when flow-induced vibration is a concern.
Thermal Expansion Can Decide the Mechanical Configuration
The shell and tube bundle may operate at different metal temperatures and may not expand by the same amount. That relative movement has to be considered before the exchanger configuration is finalized.
If relative movement is restrained, thermal stresses can develop in the tubes, tubesheets, shell and associated joints.
What actually influences the expansion check?
The shell and tubes respond to the temperature of the metal itself, not only the fluid inlet temperature.
Different materials can have different thermal expansion characteristics.
Longer effective lengths can create greater total dimensional change for the same temperature shift.
Normal operation is only one condition the exchanger may experience.
Transient conditions can create a different temperature relationship than steady-state operation.
The way the shell and bundle are restrained changes how thermal movement turns into stress.
Different configurations handle relative movement differently.
Differential expansion has to be checked carefully because the tubesheets are fixed to the shell.
Depending on the service and mechanical design, an expansion joint may be considered to accommodate shell-side movement.
Individual tubes can flex as the bundle expands and contracts, which can reduce restraint from differential expansion.
The floating end allows relative movement while also supporting a removable-bundle maintenance strategy.
An exchanger that is acceptable at steady-state operation may experience a different thermal condition during start-up, shutdown or upset conditions.
Thermal Design ≠ Mechanical Design
Meeting the heat duty is only the beginning. A practical shell-and-tube heat exchanger has to move from thermal performance into hydraulic, maintenance and mechanical decisions before it is ready to manufacture.
Define the required heating, cooling, condensing or heat-recovery load.
Hot- and cold-side inlet / outlet conditions define the thermal target.
Area follows from duty, temperature driving force, heat-transfer behavior and fouling assumptions.
Tube count, passes and flow area directly change velocity.
Thermal improvement is not useful if the system cannot supply the required ΔP.
Long-term cleanliness and maintenance access belong in the design basis.
Tube support and shell-side flow conditions need to be reviewed together.
Differential movement may influence the exchanger configuration itself.
Shell, tubesheets, channels, nozzles, supports, joints and other components follow the complete design conditions.
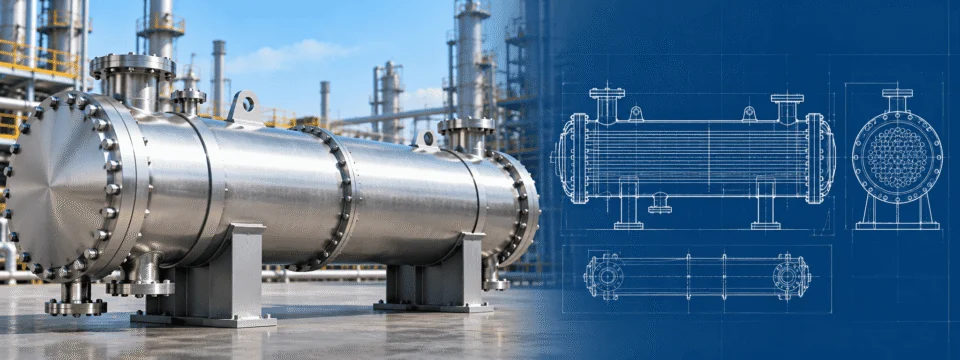
Can the required duty be achieved?
Can the equipment survive and be maintained?
Thermal performance, pressure drop, fouling, cleaning, vibration, expansion and mechanical construction have to work as one design.
Materials and Construction Options
The same material does not need to be used everywhere. Shell, tubes, tubesheet, channels and internal components can be selected around the fluid contacting each part, corrosion mechanism, pressure, temperature and project specification.
Different parts of the exchanger can solve different material problems.
Fitting more tubes into the shell is not the only objective.
Tube arrangement affects shell-side flow, heat-transfer density, pressure drop and the ability to clean between tubes. The preferred pattern depends on what the service needs.
Can provide compact tube density and strong shell-side crossflow characteristics.
Can provide more direct cleaning lanes when shell-side mechanical cleaning matters.
The joint method should match the service, not habit.
Mechanical expansion can be used where the service and leakage requirements allow it.
Welding can be considered where pressure, leakage risk or service conditions justify it.
Combined construction can be selected where both sealing and mechanical requirements need to be addressed.
Cyclic service, corrosion, code requirements and customer specifications can change the preferred joint detail.
Horizontal or vertical installation can be engineered around the process.
Orientation can influence drainage, venting, phase behavior, plant layout and maintenance access.
Nozzles and flanges should fit the plant — not a fixed catalog drawing.
Nozzle size, flange standard, orientation and instrument connections can be integrated with the project piping layout.
One Mechanical Platform, Very Different Process Duties
Shell-and-tube construction can be adapted across many industries, but the exchanger should follow the actual fluid, phase behavior, pressure, fouling tendency and maintenance requirement of each service.

Chemical Industry
Corrosion, fouling and cleaning can dominate material selection, fluid allocation and exchanger configuration.

Petrochemical Industry
Pressure, temperature, allowable ΔP and heat-recovery targets can strongly influence area, passes and mechanical design.
Oil & Gas
Pressure containment, phase behavior and field maintenance constraints can drive fluid allocation and configuration.

Pharmaceutical Industry
Material selection, cleanability, surface requirements and project documentation may become more specific.

Food & Beverage
The construction should match whether the exchanger is used for utility service or product-contact service.
Power and Industrial Utilities
Reliability, pressure drop and long operating periods often dominate the balance between performance and maintainability.
A similar-looking exchanger can require a very different tube material, pass arrangement, baffle design, cleaning strategy or mechanical configuration when the service changes.
A Good Thermal Design Still Has to Be Built Correctly
A shell-and-tube exchanger combines pressure-retaining components, thin heat-transfer tubes, numerous tube-to-tubesheet joints, internal supports and accurately positioned nozzles. Fabrication control matters at every stage.
What is checked from material receipt to final documentation?
Material identity and traceability
Material identification and traceability can be maintained according to the applicable project and code requirements.
Pressure-retaining weld execution
Pressure-retaining welds are produced according to the applicable welding procedures and agreed project requirements.
One of the most critical exchanger interfaces
Joint preparation, expansion or welding sequence and final inspection should follow the selected tube-to-tubesheet construction method.
Interfaces have to match the plant layout
Key dimensions can be checked against the approved drawing and agreed fabrication tolerances.
Examination scope follows the project basis
Depending on code, material and project specification, suitable non-destructive examination methods can be incorporated into the inspection plan.
Final pressure boundary verification
Hydrostatic testing and, where specified and permitted by the applicable code and approved procedure, pneumatic or additional leak-testing methods can be incorporated.
Dimensions that matter after the exchanger arrives on site
Must align with the connected piping arrangement.
Must match foundations, steelwork and installation geometry.
Influence assembly, shell clearance and maintenance access.
Important to the selected tube-to-tubesheet joint detail.
Connects fabrication accuracy with the thermal and mechanical design.
Affects transport, installation and maintenance clearance.
Quality control should leave a usable record.
A documentation package can be prepared around the agreed project scope, combining relevant drawings, material records, inspection results and test documentation.
What We Need to Size Your Heat Exchanger
“20 m² heat exchanger” is not enough information. Heat-transfer area is an output of the design process, not the only input.
If you already have a completed exchanger datasheet or drawing, send it for review. If you are starting from process conditions, the information below gives us a much stronger basis for thermal and mechanical engineering.
Hot Side and Cold Side Data Should Be Defined Separately
Property data improves the quality of the thermal calculation.
If these values are available from your process data, include them for each stream. They can materially change heat-transfer and pressure-drop calculations.
Influences velocity and hydraulic behavior.
Affects Reynolds number, pressure drop and heat transfer.
Connects flow rate with the required heat duty.
Influences convective heat-transfer behavior.
Important for condensing, boiling and mixed-phase service.
Can change fouling risk, velocity limits and cleaning strategy.
Thermal data alone does not define the equipment.
Maximum / minimum mechanical design conditions.
Required or prohibited materials and alloy preferences.
Applicable code or customer specification where already defined.
Fixed, U-tube, floating head or existing replacement basis if specified.
Horizontal / vertical and installation constraints.
Plant piping interface and connection requirements.
Mechanical, chemical, CIP or maintenance strategy.
Bundle pull space, lifting access and surrounding equipment.
NDE / NDT, witness points or customer inspection scope.
Drawings, material records, inspection and test documents.
Indoor, outdoor, corrosive atmosphere or other site conditions.
Nameplate, old drawing or current operating data for replacement projects.
Send what you already have.
A process datasheet, PFD, P&ID, existing exchanger nameplate, drawing or current operating conditions can help establish the next engineering questions.
Frequently Asked Questions About Shell and Tube Heat Exchangers
These questions usually appear before quotation because configuration, cleaning, pressure drop, materials and maintenance requirements can change the exchanger significantly.
Which is better: fixed tubesheet, U-tube or floating head?
None is automatically better. Fixed tubesheet exchangers provide relatively simple construction, U-tube exchangers accommodate differential expansion efficiently, and floating-head exchangers provide strong maintenance access and thermal movement capability.
The correct choice depends on fouling, cleaning requirements, temperature difference, pressure, fluid allocation and maintenance strategy.
Can you manufacture from an existing drawing?
Yes. Existing drawings and datasheets can be used as the starting point for quotation and engineering review.
Important design conditions should still be checked before fabrication, especially when the existing exchanger has recurring fouling, corrosion, vibration or performance problems.
Can shell and tube heat exchangers be customized?
Yes. Shell diameter, tube length, tube material, shell material, tubesheet construction, number of passes, baffle arrangement, nozzle orientation, support arrangement and overall configuration can be adapted to the project requirements.
Final geometry should follow the process and mechanical design rather than a catalog size alone.
What materials can be used?
Common project materials include carbon steel and stainless steels such as 304/304L and 316/316L.
Duplex stainless steel, titanium and other project-specified alloys can also be considered where corrosion conditions justify them. Different materials can be used for the shell, tubes, tubesheet and channels when appropriate.
How do I know whether the tube bundle needs to be removable?
Consider what happens when the exchanger becomes fouled. If the shell side requires mechanical access to the outside of the tubes, a removable bundle may be important.
If chemical cleaning is acceptable and the service is relatively clean, bundle removal may be less important. The available extraction space at the installation site must also be checked.
Does more heat-transfer area always improve performance?
No. Additional surface area can provide thermal margin, but changing the number of tubes can also change fluid velocity and pressure drop.
If velocity becomes too low, the exchanger may become more susceptible to fouling in some services. Area, velocity, pressure drop and fouling should therefore be evaluated together.
Why is allowable pressure drop important?
Pressure drop is part of the energy required to move fluid through the exchanger.
A geometry that provides strong heat transfer may still be unsuitable if the pump or process cannot supply the required pressure. Providing allowable ΔP on both shell side and tube side gives the designer much more freedom to optimize the exchanger correctly.
Can you design for high-pressure or high-temperature service?
Shell-and-tube exchangers can be engineered for demanding pressure and temperature conditions, but there is no useful universal pressure or temperature limit for a custom exchanger.
The practical design depends on material, diameter, wall thickness, joint design, tubesheet design, configuration, applicable code and the complete operating conditions.
Send Us the Operating Conditions — Not Just the Required Area
A shell-and-tube heat exchanger should balance heat duty, pressure drop, fluid velocity, fouling, corrosion, cleaning, thermal expansion and mechanical design.
Send your process conditions, existing datasheet or equipment drawing. We can use that information to define the exchanger configuration and manufacturing requirements around the actual service.
Hot side and cold side media
Mass or volumetric flow
Inlet and required outlet conditions
Pressure and temperature basis
Shell-side and tube-side limits
Maintenance and deposit behavior